In the demanding world of industrial fluid management, the ability to move high-density solids without clogging is a critical operational challenge. A submersible slurry pump with agitator represents a specialized engineering solution designed to handle abrasive materials, ensuring that settled solids are resuspended and transported efficiently. By combining powerful suction with active agitation, these systems minimize downtime and maximize throughput in the toughest environments.
Globally, the demand for robust slurry handling has surged as mining, dredging, and waste management industries scale their operations. The integration of a submersible slurry pump with agitator allows operators to maintain a consistent flow of high-concentration slurries, preventing the common issue of "sanding in" where heavy particles solidify around the pump intake. This capability is essential for maintaining the continuity of industrial supply chains and environmental remediation projects.
Understanding the technical nuances of these pumps—from material selection like hyper chrome alloys to hydraulic design—is key to optimizing operational costs. Whether it is feeding a filter press or clearing a sump, the right configuration of a submersible slurry pump with agitator ensures that wear is minimized and energy efficiency is maximized, providing a sustainable long-term solution for heavy-duty slurry transport.
Global Industrial Relevance of Slurry Agitation
On a global scale, the management of abrasive slurries is a multi-billion dollar challenge affecting infrastructure and resource extraction. According to industrial standards, the efficiency of waste transport in mining and chemical processing depends heavily on the pump's ability to handle high solids concentrations—often up to 60%. The use of a submersible slurry pump with agitator prevents the sedimentation of heavy particles, which otherwise leads to costly pipeline blockages and pump failures.
In regions with heavy industrialization, such as East Asia and North America, the move toward automated slurry handling has highlighted the need for pumps that can operate submerged without the constant need for manual clearing. By integrating agitation directly into the suction process, industries reduce labor costs and improve safety by minimizing the need for personnel to enter hazardous sump areas.
Defining the Submersible Slurry Pump with Agitator
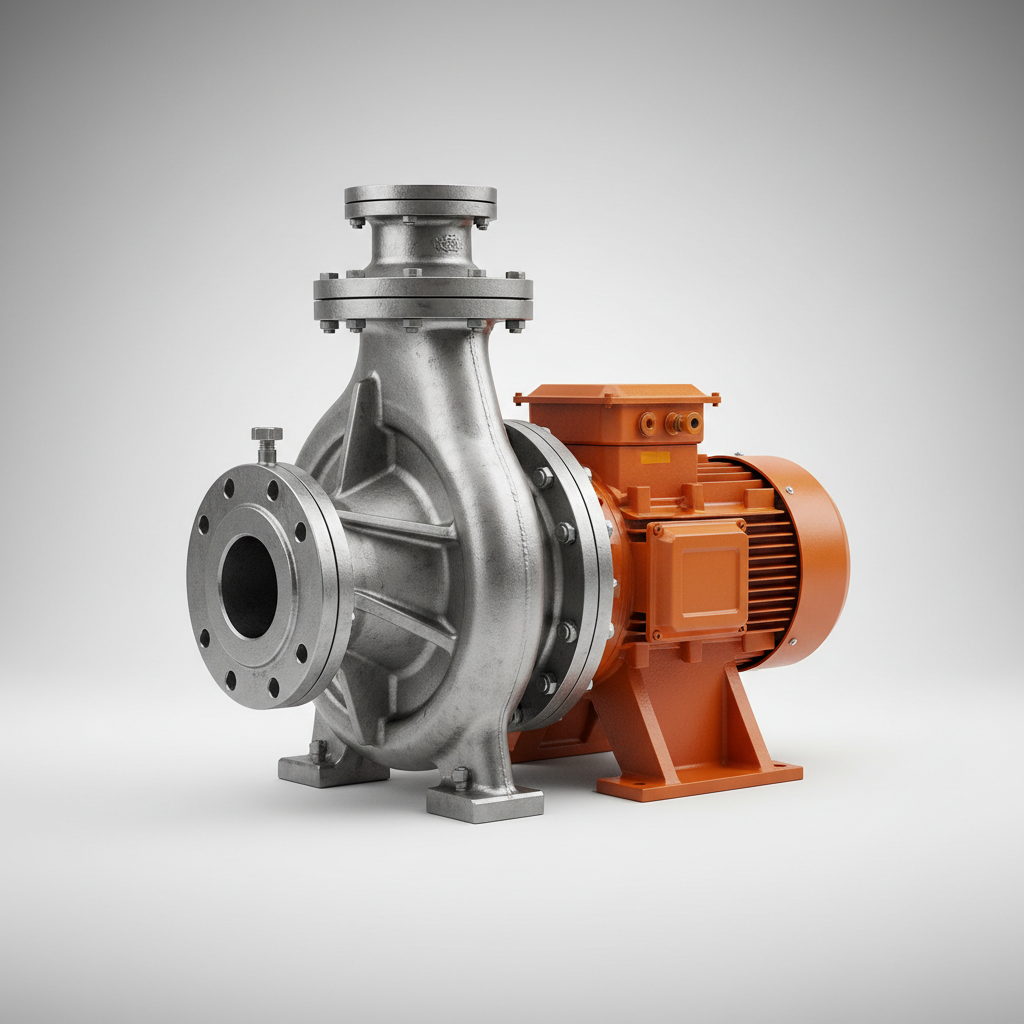
A submersible slurry pump with agitator is a heavy-duty centrifugal pump designed to be fully immersed in the fluid it pumps. Unlike standard water pumps, these units are engineered to transport liquids containing high concentrations of suspended solids—such as sand, gravel, and mineral ores. The "agitator" component is a rotating mechanism at the suction end that stirs up settled solids, transforming a thick, static sludge into a pumpable slurry.
From a technical standpoint, these pumps are characterized by their ability to handle varying concentrations (from 0% to 60%) and significant solid sizes (up to 70mm). This makes them indispensable for humanitarian and environmental efforts, such as cleaning contaminated riverbeds or managing wastewater in flood-prone urban areas, where the mixture of water and debris is unpredictable.
The synergy between the submersible motor and the agitation system allows for a compact footprint and eliminates the need for complex suction lift calculations. By placing the pump directly in the medium, the risk of cavitation is reduced, and the efficiency of solids intake is significantly increased compared to surface-mounted alternatives.
Core Components for Maximum Durability
The longevity of a submersible slurry pump with agitator depends primarily on the materials used in its construction. Given the abrasive nature of slurries, manufacturers utilize Hyper Chrome alloys and high-grade Ceramics to line the volute and impeller. These materials provide the necessary hardness to resist the constant scouring effect of mineral particles.
A critical feature of the submersible slurry pump with agitator is the sealing mechanism. While many industrial pumps rely on complex mechanical seals that require external water cooling, specialized designs utilize packing glands that guarantee no leakage while remaining simple to maintain, reducing the overall operational complexity.
Furthermore, the hydraulic design is optimized for "sharp" capacity/head curves. This ensures that the submersible slurry pump with agitator can start with high capacity and low pressure and transition to low capacity and high pressure as the process evolves, making it ideal for feeding filter presses where pressure requirements change over time.
Performance Metrics and Hydraulic Efficiency
Analyzing the efficiency of a submersible slurry pump with agitator requires a look at the relationship between flow rate (m3/h) and head (m). For instance, in a range of sizes from 65mm to 125mm, these pumps can achieve capacities from 40 to 304 m3/h. The ability to adjust impeller diameters allows operators to fine-tune the pump to their specific pressure requirements without needing expensive frequency converters.
The operational stability is further enhanced by the use of standardized motors (such as the Y series), ensuring that the shaft power is balanced against the density of the slurry. When pumping high-density materials, maintaining a short inlet pipe is crucial to prevent suction losses and ensure the agitator can effectively feed the impeller.
Efficiency Comparison of Slurry Agitation Methods
Real-World Applications in Heavy Industry
The versatility of the submersible slurry pump with agitator makes it a staple in mining operations. In tailings ponds, where solids naturally settle over time, these pumps are used to dredge and transport slurry back to processing plants. Their ability to handle solids up to 70mm means they can manage not just fine silt, but also larger rocky debris that would destroy standard pumps.
Beyond mining, these pumps are essential in municipal wastewater treatment and industrial filter press feeding. In a filter press application, the pump must move high-density sludge into a press under increasing pressure. The specific hydraulic design of the submersible slurry pump with agitator allows it to adapt to these changing pressure profiles, ensuring the filter plates are filled evenly and efficiently.
Long-Term Value and Operational Sustainability
Investing in a high-quality submersible slurry pump with agitator provides immense long-term value by reducing the "Total Cost of Ownership." While the initial investment in hyper chrome or ceramic materials is higher, the extended intervals between maintenance shutdowns far outweigh the upfront cost. Reliability in a submersible slurry pump with agitator means fewer unplanned outages and a safer work environment.
Sustainability is also a key factor. By optimizing the flow of high-density slurries, these pumps reduce the amount of water required for transport, thereby lowering the overall environmental footprint of the operation. The energy efficiency gained from advanced hydraulic designs means lower electricity consumption per cubic meter of material moved.
Moreover, the ease of installation—specifically the option for belt-pulley coupling and flood suction—allows these pumps to be integrated into existing infrastructures with minimal modification. This adaptability ensures that companies can upgrade their slurry handling capabilities without needing to redesign their entire piping network.
Future Innovations in Slurry Handling Technology
The future of the submersible slurry pump with agitator is leaning toward "Smart Pumping." Integration with IoT sensors will allow operators to monitor wear in real-time, predicting exactly when a liner needs replacement based on flow turbulence and vibration analysis. This shift from reactive to predictive maintenance will further minimize downtime.
Material science is also evolving, with the introduction of nano-ceramic composites that offer even greater hardness than current hyper chrome alloys. These materials will allow the submersible slurry pump with agitator to handle even more corrosive and abrasive chemicals, expanding its use into the advanced pharmaceutical and chemical synthesis industries.
Lastly, the move toward green energy is prompting the development of higher-efficiency motors that maintain torque at lower RPMs. This will allow for more precise control over the agitation process, ensuring that only the necessary amount of energy is used to resuspend solids, further enhancing the sustainability of industrial slurry transport.
Technical Specifications and Selection Matrix for Slurry Pumps
|
Pump Model/Size
|
Max Capacity (m3/h)
|
Max Head (m)
|
Handling Solids (mm)
|
| 65WYLT |
41.4 - 80.0 |
55.2 - 69.0 |
Up to 70mm |
| 80WYLT |
60.0 - 133.0 |
76.0 - 115.0 |
Up to 70mm |
| 100WYLT |
85.0 - 175.0 |
73.3 - 169.0 |
Up to 70mm |
| 125WYLT (Type A) |
105 - 265 |
73.5 - 245 |
Up to 70mm |
| 125WYLT (Type B) |
119 - 305 |
80.0 - 279 |
Up to 70mm |
| 125WYLT (High Head) |
87.0 - 215 |
91.8 - 203 |
Up to 70mm |
FAQS
The primary advantage is the integrated agitator, which actively stirs settled solids at the bottom of a sump. Standard pumps often clog or "sand in" when faced with high-density slurries; the agitator ensures a consistent flow of material into the impeller, reducing downtime and preventing the need for manual dredging of the pump intake.
For highly abrasive environments, Hyper Chrome alloys and Ceramic linings are the gold standard. These materials provide extreme hardness and wear resistance, significantly extending the life of the impeller and volute compared to standard cast iron or stainless steel, which would erode quickly under the impact of mineral particles.
The current specifications for this series of submersible slurry pumps with agitators are designed for solids up to 70mm. Attempting to pump larger solids may lead to impeller blockages or internal damage. For larger debris, a specialized trash pump or a larger custom-engineered slurry pump would be required.
No, a frequency converter is not strictly necessary. Depending on the application, the pump speed can be adjusted by cutting the impeller diameter or utilizing a belt-pulley coupling system. This allows the pump to meet specific head and capacity requirements through mechanical adjustments rather than electrical ones.
Packing glands are often preferred in heavy slurry applications because they are simpler and more robust. Unlike mechanical seals, which can be easily damaged by abrasive particles getting trapped between the seal faces, a packing gland is more forgiving and can be maintained or replaced more easily without dismantling the entire pump.
Flood suction is highly suggested for high-density slurry due to its low suction head requirements. Additionally, to avoid affecting suction efficiency, it is critical that the inlet pipe is kept as short as possible and that the suction/discharge pipe diameter is equal to or larger than the pump's diameter.
Conclusion
The submersible slurry pump with agitator is an essential tool for any industry dealing with high-concentration solids. By combining durable materials like hyper chrome alloys with an active agitation system, these pumps solve the critical problem of sedimentation and clogging. From the technical precision of their hydraulic curves to the robustness of their packing gland seals, every element is designed to maximize uptime and reduce the total cost of ownership in the most abrasive environments.
As industrial operations move toward greater automation and environmental sustainability, the role of efficient slurry handling will only increase. We recommend that operators carefully analyze their solids concentration and particle size to select the optimal pump size and material. By investing in high-efficiency agitation technology today, industries can ensure a more reliable, safe, and cost-effective operational future. Visit our website for more details: www.aierpumps.com