In the demanding world of industrial mining and mineral processing, the efficiency of fluid transport determines the overall productivity of the operation. The search for a reliable wholesale medium head heavy duty slurry pump is often driven by the need to move highly abrasive materials—such as tailings, ore slurries, and chemical waste—across moderate elevations without sacrificing equipment longevity.
Achieving the perfect balance between "medium head" pressure and "heavy duty" durability requires precision engineering, particularly in the sealing and impeller components. When organizations look for wholesale solutions, they aren't just buying hardware; they are investing in the reduction of downtime and the optimization of their slurry handling lifecycle, ensuring that abrasive particles do not compromise the structural integrity of the pump.
Understanding the intricacies of these systems, from the choice of materials to the specific role of the expeller ring in maintaining shaft seals, allows plant managers to maximize throughput. This guide explores the technical and commercial landscape of the wholesale medium head heavy duty slurry pump, providing a comprehensive overview of how these machines power the global extractive and processing industries.
Global Significance of Slurry Pumping Systems
Across the globe, the extraction of minerals and the processing of industrial waste rely heavily on the ability to transport dense, abrasive fluids. The demand for a wholesale medium head heavy duty slurry pump has surged as mining operations move toward deeper deposits and more complex processing plants that require consistent pressure to move material over moderate distances.
From the copper mines of Chile to the gold fields of Australia, the reliability of these pumps is a critical KPI for operational success. Failure in a single pump unit can lead to catastrophic bottlenecks, highlighting the need for heavy-duty specifications that can withstand the relentless wear of slurry particles while maintaining a steady head of pressure.
Defining the Medium Head Heavy Duty Standard
In technical terms, a "medium head" slurry pump is designed to provide a pressure range that is higher than standard transfer pumps but lower than high-pressure multistage systems. This makes it the ideal choice for moving slurry from a primary sump to a processing tank or through a moderate pipeline network. When combined with "heavy duty" specifications, it implies the use of premium alloys and reinforced seals to combat erosion and corrosion.
The "wholesale" aspect of these procurement strategies allows large-scale mining and dredging firms to standardize their fleets. By sourcing consistent models, such as those compatible with B-AH or C-AH series designs, companies can reduce their inventory of spare parts and ensure that maintenance crews are trained on a unified system, thereby reducing the Mean Time To Repair (MTTR).
Ultimately, the medium head heavy duty standard is about balancing energy consumption with raw power. It ensures that the fluid velocity is high enough to keep solids in suspension—preventing pipe blockages—without creating excessive turbulence that would accelerate the wear on the pump's internal liners and impellers.
Core Components: The Role of the Expeller Ring
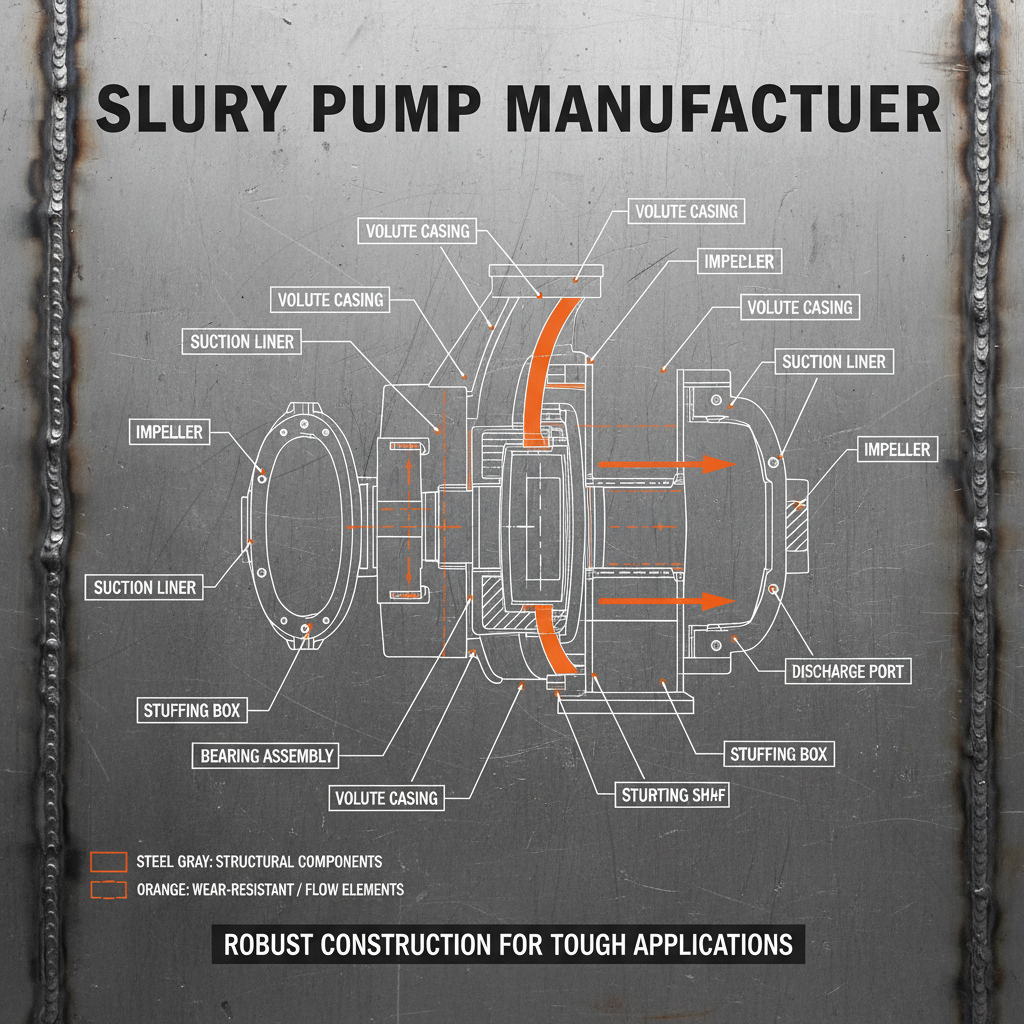
The heart of a wholesale medium head heavy duty slurry pump lies in its ability to seal the shaft against abrasive ingress. This is where the expeller ring becomes indispensable. The expeller ring is a critical component that, when combined with the expeller, forms an expeller seal—one of the three primary types of slurry pump shaft seals.
For specific models such as the B029 (1.5/1B-AH, 2/1.5B-AH) or the CSC029 (75C-L), the expeller ring 029 serves as the primary barrier. It works by creating a centrifugal force that pushes the slurry away from the shaft seal area, effectively reducing the amount of abrasive material that reaches the gland packing or mechanical seal, which significantly extends the pump's operational life.
Whether dealing with the H029 (16/14TU-AH) or the EAM029 (10/8E-M) models, the precision of the expeller ring's fit is what separates a standard pump from a heavy-duty one. By ensuring that the seal remains intact under medium head pressures, the expeller ring prevents costly leaks and protects the pump's bearings from contamination.
Performance Metrics and Efficiency Factors
Evaluating a wholesale medium head heavy duty slurry pump requires looking beyond the flow rate. Key metrics include the Net Positive Suction Head (NPSH), the wear rate of the high-chrome liners, and the efficiency of the expeller seal in preventing slurry leakage. High-performance pumps are characterized by their ability to maintain a steady head even as the viscosity of the slurry changes.
The integration of the expeller ring 029 across various pump sizes—from the smaller B029 to the massive H029—ensures a scalable performance curve. By optimizing the gap between the expeller and the ring, engineers can maximize the "pumping out" effect, ensuring that the pump maintains its heavy-duty rating even under continuous 24/7 operation in harsh environments.
Efficiency Ratings of Wholesale Medium Head Heavy Duty Slurry Pump Variants
Global Industrial Applications and Use Cases
The versatility of the wholesale medium head heavy duty slurry pump allows it to be deployed across diverse sectors. In the mining industry, these pumps are essential for tailings management, where they move waste solids to storage facilities. The use of specific expeller ring models, such as the DSC029 for 100D-L pumps, ensures that these systems can handle the grit and sand of mine tailings without frequent seal failures.
Beyond mining, these pumps are critical in Flue Gas Desulfurization (FGD) plants in power stations, where they handle gypsum slurries. In these chemical-heavy environments, the "heavy duty" aspect is not just about abrasion but also about corrosion resistance. Whether it is a 6/4D-G model in a sand dredging project or a 14/12ST-AH in a wastewater treatment facility, these pumps provide the necessary head to ensure smooth fluid transport.
Long-Term Value and Sustainability Benefits
Investing in a high-quality wholesale medium head heavy duty slurry pump offers significant long-term economic value. By selecting pumps with superior components—like the expeller ring 029—operators reduce the frequency of unplanned shutdowns. In the slurry industry, downtime is often more expensive than the equipment itself, making reliability the primary driver of ROI.
From a sustainability perspective, efficient medium head pumps reduce the energy footprint of the entire plant. By optimizing the flow dynamics and reducing internal friction and leakage through advanced sealing, these pumps lower the kWh required per ton of material moved. This contributes to a more green industrial operation, aligning with global ISO standards for energy efficiency.
Furthermore, the ability to source standardized spare parts wholesale ensures that equipment remains operational for decades rather than years. The modularity of the AH and HH series allows for easy upgrades and replacements, promoting a circular economy where components are refurbished rather than scrapped.
Future Innovations in Slurry Technology
The evolution of the wholesale medium head heavy duty slurry pump is moving toward "smart pumping." Integration of IoT sensors into the expeller seal assembly will soon allow for real-time monitoring of wear. Instead of scheduled maintenance, operators will move to predictive maintenance, replacing the expeller ring only when the sensor detects a drop in sealing efficiency.
Material science is also playing a pivotal role. The development of new ceramic composites and nano-coatings is expected to replace traditional high-chrome irons in some applications. This will further enhance the "heavy duty" capabilities of pumps, allowing them to handle even more corrosive or abrasive slurries while maintaining the same medium head pressure.
As automation increases, we will see pumps that can automatically adjust their speed based on the slurry density, optimizing energy use in real-time. This digital transformation will ensure that the wholesale market for slurry pumps continues to grow, providing more tailored and efficient solutions for the world's most challenging industrial environments.
Technical Specifications and Compatibility Analysis of Slurry Pump Components
|
Pump Model Series
|
Expeller Ring Code
|
Application Type
|
Wear Resistance Score (1-10)
|
| B-AH (1.5/1B) |
B029 |
Light Industrial Slurry |
7.5 |
| C-AH (3/2C) |
C029 |
Medium Mining Tailings |
8.2 |
| D-AH (4/3D) |
D029 |
Heavy Gravel/Sand |
9.0 |
| E-AH (6/4E) |
E029 |
High Density Ore |
9.5 |
| F-AH (8/6F) |
F029 |
Large Volume Transfer |
8.8 |
| H-AH (16/14TU) |
H029 |
Ultra Heavy Duty/High Head |
9.8 |
FAQS
The expeller ring works in conjunction with the expeller to form an expeller seal. Its primary role is to create a centrifugal barrier that pushes abrasive slurry away from the shaft seal area. This prevents solids from entering the seal housing, which drastically reduces wear on the packing or mechanical seals and prevents leakage in a wholesale medium head heavy duty slurry pump.
The 029 expeller ring is highly versatile and compatible with a wide range of models including B029 (1.5/1B-AH), C029 (3/2C-AH), D029 (4/3D-AH), E029 (6/4E-AH), and the high-capacity H029 (16/14TU-AH). It is also used in L-series pumps such as the BSC029 (50B-L) and CSC029 (75C-L).
Medium head pumps are more energy-efficient for applications that do not require extreme elevation changes. They provide enough pressure to maintain the critical carrying velocity of the slurry to prevent settling, without the excessive energy costs and higher wear rates associated with high-head pumps.
Replacement intervals depend on the slurry's abrasiveness. However, in heavy-duty mining environments, it is recommended to inspect the expeller ring during every scheduled impeller check. A worn ring will allow slurry to bypass the seal, leading to rapid failure of the shaft sleeve and bearings.
While the 029 code refers to a specific design standard, you must ensure the specific model code (e.g., B029 vs H029) matches your pump's physical dimensions. While they share the same functional logic, the diameters vary across the AH and HH series to fit different shaft sizes.
Not when sourcing from reputable manufacturers. Wholesale procurement usually implies standardized production, which actually ensures higher quality consistency. Components like the expeller ring 029 are manufactured to strict tolerances to ensure they fit perfectly across thousands of units.
Conclusion
The operational success of any slurry-handling facility hinges on the durability and efficiency of its pumping infrastructure. From the critical role of the expeller ring in maintaining the seal integrity of models like the B029 and H029 to the strategic advantage of sourcing a wholesale medium head heavy duty slurry pump, every technical detail contributes to reduced downtime and lower operational costs. By balancing pressure requirements with heavy-duty material science, industries can ensure a seamless flow of materials even in the harshest environments.
Looking forward, the integration of smart monitoring and advanced composite materials will further elevate the standards of slurry transport. We encourage plant managers and procurement specialists to prioritize the quality of sealing components and standardize their equipment fleets to maximize long-term reliability. For more information on high-performance slurry solutions, visit our website: www.aierpumps.com