The industrial landscape for fluid handling has evolved rapidly, placing a premium on equipment that can withstand the most abrasive environments. Among these, the oem horizontal slurry pump stands as a cornerstone for mining, dredging, and chemical processing, where the movement of thick, particle-laden liquids is a daily necessity. Understanding the engineering behind these machines is crucial for optimizing operational uptime and reducing long-term maintenance costs.
Across the globe, the demand for high-performance pumping solutions has surged as mineral extraction and waste management processes become more complex. The challenge lies in balancing flow efficiency with the inevitable wear and tear caused by suspended solids. This is where the strategic implementation of an oem horizontal slurry pump becomes vital, ensuring that heavy-duty industrial processes remain uninterrupted and cost-effective.
By leveraging advanced casting materials and precise OEM specifications, industries can significantly extend the lifecycle of their machinery. Investing in a high-quality oem horizontal slurry pump ensures that the equipment is tailored to the specific density and chemistry of the slurry, preventing premature failure and enhancing overall plant productivity.
Material Science in OEM Slurry Pump Casting
The longevity of an oem horizontal slurry pump is fundamentally tied to the materials used in its casting. Depending on the application, manufacturers utilize a diverse array of alloys, including high chrome white iron for extreme abrasion resistance, and stainless steel for corrosive environments. The ability to produce castings ranging from 1kg to 20MT allows for immense flexibility in pump sizing and component replacement.
Furthermore, the use of ductile iron and grey iron provides the necessary structural integrity for pump housings and frames. By selecting the correct anti-wear steel, an oem horizontal slurry pump can maintain its hydraulic efficiency even when transporting highly aggressive tailings or gravel-laden water, reducing the frequency of costly shutdowns.
Understanding the Design of Horizontal Slurry Pumps
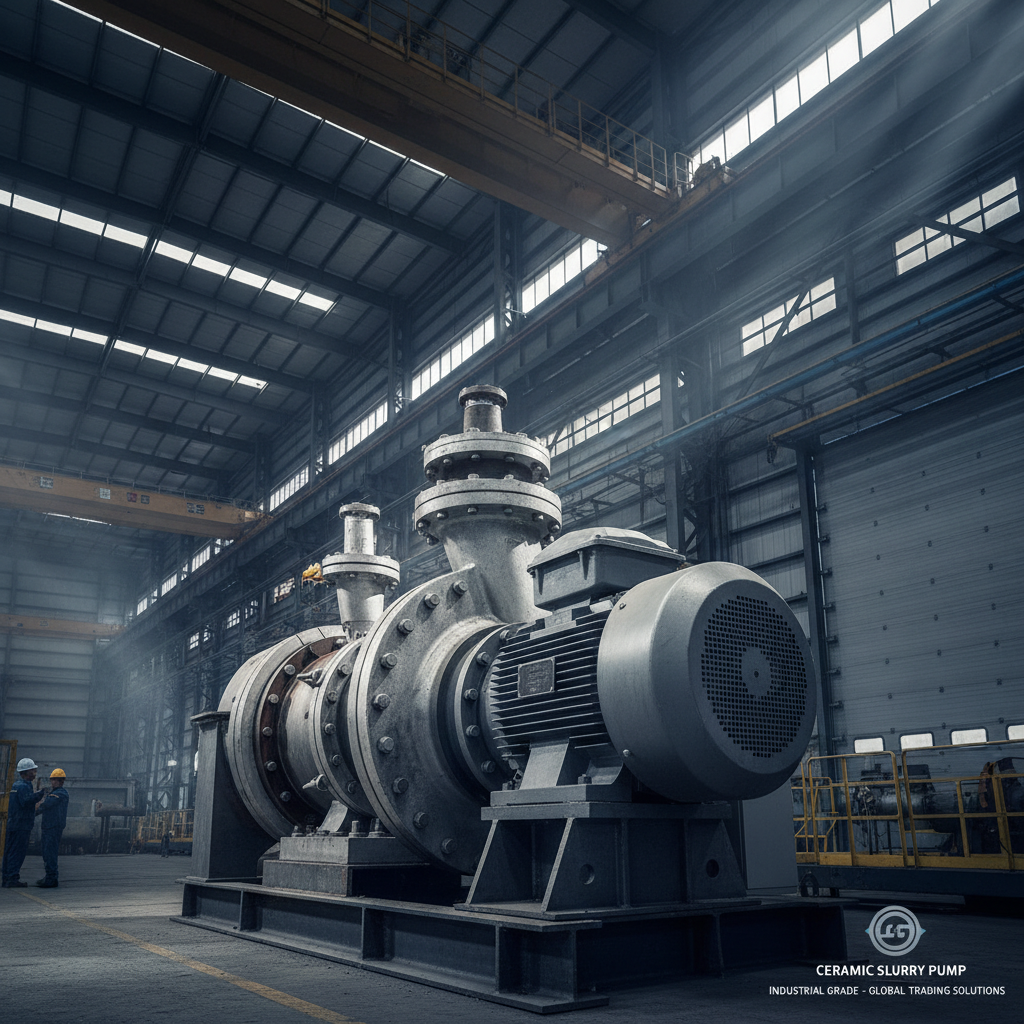
The horizontal configuration of these pumps is specifically designed to facilitate easier maintenance and installation within industrial plants. By placing the drive shaft and impeller on a horizontal plane, operators can more easily access the wear parts for inspection and replacement without dismantling the entire piping system.
From an engineering perspective, the oem horizontal slurry pump focuses on minimizing turbulence and maximizing flow velocity to prevent the settling of solids within the pump casing. This design ensures a consistent flow rate, which is critical for processes like froth flotation or mineral leaching where precise concentration levels are required.
OEM customization allows for the adjustment of impeller diameters and casing thicknesses based on the specific gravity of the slurry. This means that whether the application is light sewage or heavy metal ore, the pump can be optimized for the lowest possible energy consumption per cubic meter of fluid moved.
Core Components and Their Functional Roles
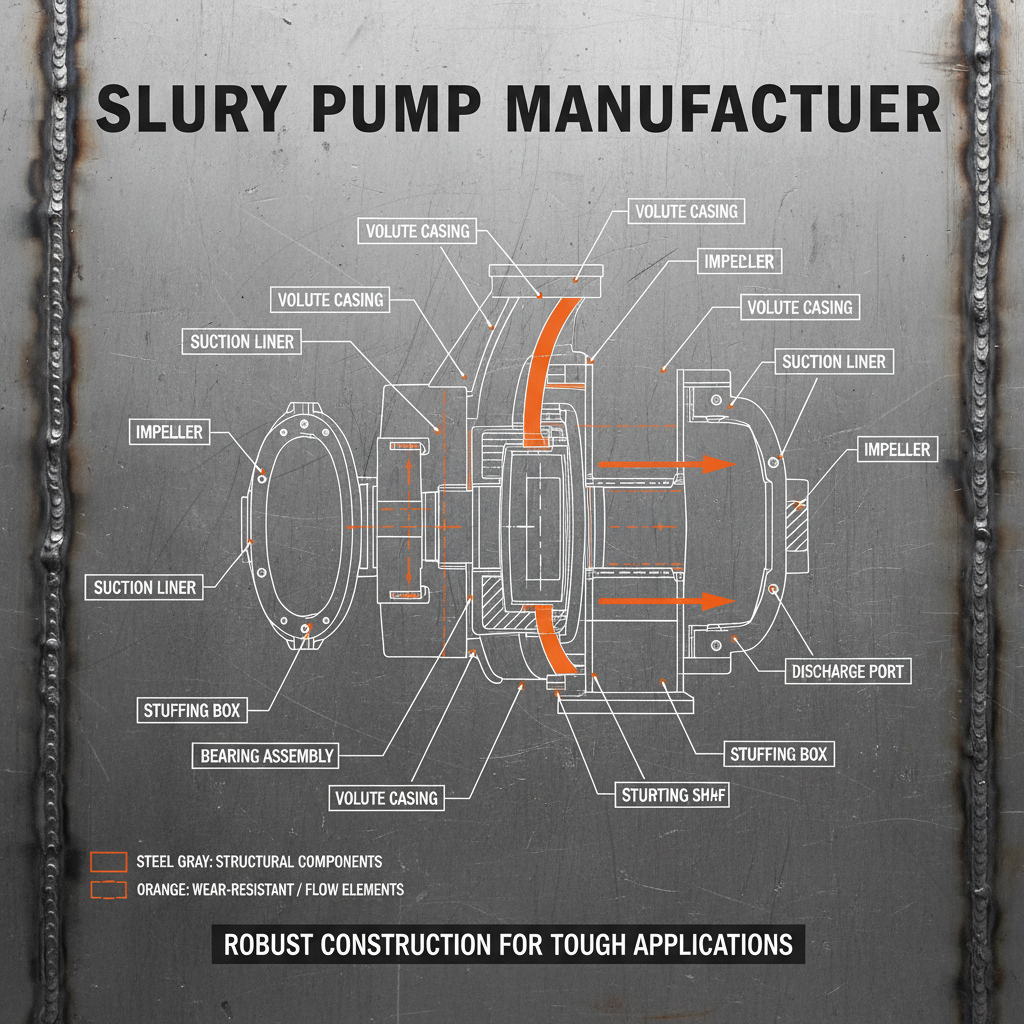
The efficiency of an oem horizontal slurry pump depends on the synergy between its impeller, volute, and liner. The impeller is the heart of the machine, accelerating the slurry and creating the pressure needed for transport, while the volute converts this kinetic energy into pressure.
Wear liners are perhaps the most critical part of an oem horizontal slurry pump, as they act as a sacrificial barrier that protects the pump casing from the abrasive force of the slurry. High-quality OEM castings in chrome iron ensure these liners last longer, reducing the total cost of ownership.
The shaft and bearing assembly must be engineered to handle the heavy radial loads associated with pumping dense materials. In a professional oem horizontal slurry pump, these components are often reinforced with anti-wear steel to prevent deflection and vibration during high-load operations.
Comparative Performance of OEM Pump Materials
Selecting the right material for an oem horizontal slurry pump is not a one-size-fits-all decision. The choice between high chrome iron and stainless steel depends entirely on whether the primary threat is physical abrasion or chemical corrosion.
Different casting materials offer varying levels of hardness and impact resistance. While high chrome white iron is unmatched in hardness, ductile iron offers better resilience against sudden impacts from large solids, making it a preferred choice for certain gravel sand pump applications.
Material Durability Rating for oem horizontal slurry pump
Global Industrial Applications and Use Cases
Across the mining regions of Australia and South America, the oem horizontal slurry pump is indispensable for moving tailings from processing plants to storage facilities. These pumps operate 24/7, handling millions of gallons of abrasive waste, which necessitates the use of high-chrome castings to maintain efficiency.
In urban infrastructure projects, such as dredging operations in Southeast Asia, these pumps are used to clear silt and sand from waterways. The adaptability of the oem horizontal slurry pump allows it to switch between different slurry densities, making it a versatile tool for civil engineering and environmental restoration.
Long-Term Value and Operational Sustainability
The true value of an oem horizontal slurry pump is realized over its entire lifecycle rather than just the initial purchase price. By utilizing precision-engineered OEM parts, companies reduce the "Mean Time Between Failures" (MTBF), which translates directly into higher profit margins and less operational downtime.
Sustainability in slurry pumping is achieved through energy optimization. A well-designed oem horizontal slurry pump reduces internal friction and cavitation, leading to lower electricity consumption. This not only lowers costs but also aligns with global corporate goals to reduce the carbon footprint of heavy industry.
Furthermore, the ability to replace individual wear components—such as liners and impellers—rather than the entire pump unit promotes a circular economy. Using durable OEM castings ensures that the core structure of the pump remains viable for decades, while only the high-wear surfaces are recycled and replaced.
Future Innovations in Slurry Handling Technology
The next generation of the oem horizontal slurry pump is moving toward "smart" pumping. Integration with IoT sensors allows operators to monitor wear levels in real-time, predicting exactly when a liner needs replacement before a catastrophic failure occurs.
Material innovation continues to push boundaries, with the development of nano-composite coatings and advanced ceramic liners. These materials aim to further increase the hardness of the oem horizontal slurry pump, potentially doubling the lifespan of components in the most aggressive acid-slurry environments.
Additionally, there is a shift toward variable frequency drives (VFDs) as a standard feature. This allows the oem horizontal slurry pump to adjust its speed based on the real-time viscosity of the fluid, ensuring the pump always operates at its Best Efficiency Point (BEP).
Core Material and Performance Analysis for OEM Slurry Pumps
| Material Type |
Abrasion Resistance |
Corrosion Resistance |
Typical Use Case |
| High Chrome Iron |
Excellent |
Moderate |
Mining Tailings |
| Stainless Steel |
Moderate |
Excellent |
Chemical Slurry |
| Ductile Iron |
Good |
Low |
Gravel/Sand Pump |
| Anti-Wear Steel |
Very High |
Moderate |
Heavy Ore Transport |
| Grey Iron |
Moderate |
Low |
General Sewage |
| Ceramic Liners |
Extreme |
High |
Ultra-Fine Abrasives |
FAQS
Depending on the application, we use high chrome white iron for maximum abrasion resistance, stainless steel for corrosive fluids, and ductile or grey iron for structural components. Anti-wear steel is also common for high-impact environments. Our casting capabilities range from 1kg to 20MT to suit any pump size.
A horizontal slurry pump is installed on a flat base, making it easier to access for maintenance and liner replacement. Vertical pumps are typically used in sump applications where the pump must be submerged or take suction from a deep pit, but they are often more complex to service.
Replacement intervals vary based on the slurry's abrasiveness and flow velocity. However, using high-quality OEM castings can significantly extend this window. We recommend regular ultrasonic thickness testing to monitor wear and schedule replacements during planned shutdowns.
Yes, provided the impeller and volute are designed with a sufficient passage area. By customizing the OEM design and using impact-resistant materials like ductile iron, these pumps can effectively move gravel, sand, and other large mineral fragments without clogging.
OEM castings are manufactured to the exact metallurgical specifications and tolerances of the original equipment. This ensures a perfect fit, optimal hydraulic balance, and predictable wear life, whereas generic parts may lead to vibration, leakage, or premature failure.
You should analyze the slurry's pH level (for corrosion) and the hardness/concentration of the solids (for abrasion). For high-pH abrasive slurries, high chrome iron is best; for acidic slurries, stainless steel is preferred. Our experts can help match the material to your specific operating conditions.
Conclusion
The oem horizontal slurry pump remains a vital piece of infrastructure for any industry dealing with abrasive fluids. By combining advanced material science—from high chrome iron to anti-wear steel—with precision OEM casting, companies can achieve a balance of durability, efficiency, and cost-effectiveness. The transition toward smart monitoring and sustainable material usage further ensures that these pumps will continue to drive industrial productivity for years to come.
To maximize your operational uptime, it is essential to prioritize quality castings and precise engineering specifications. Whether you are upgrading an existing system or designing a new plant, investing in a reliable oem horizontal slurry pump is a strategic move toward long-term sustainability and reliability. Visit our website for more information: www.aierpumps.com