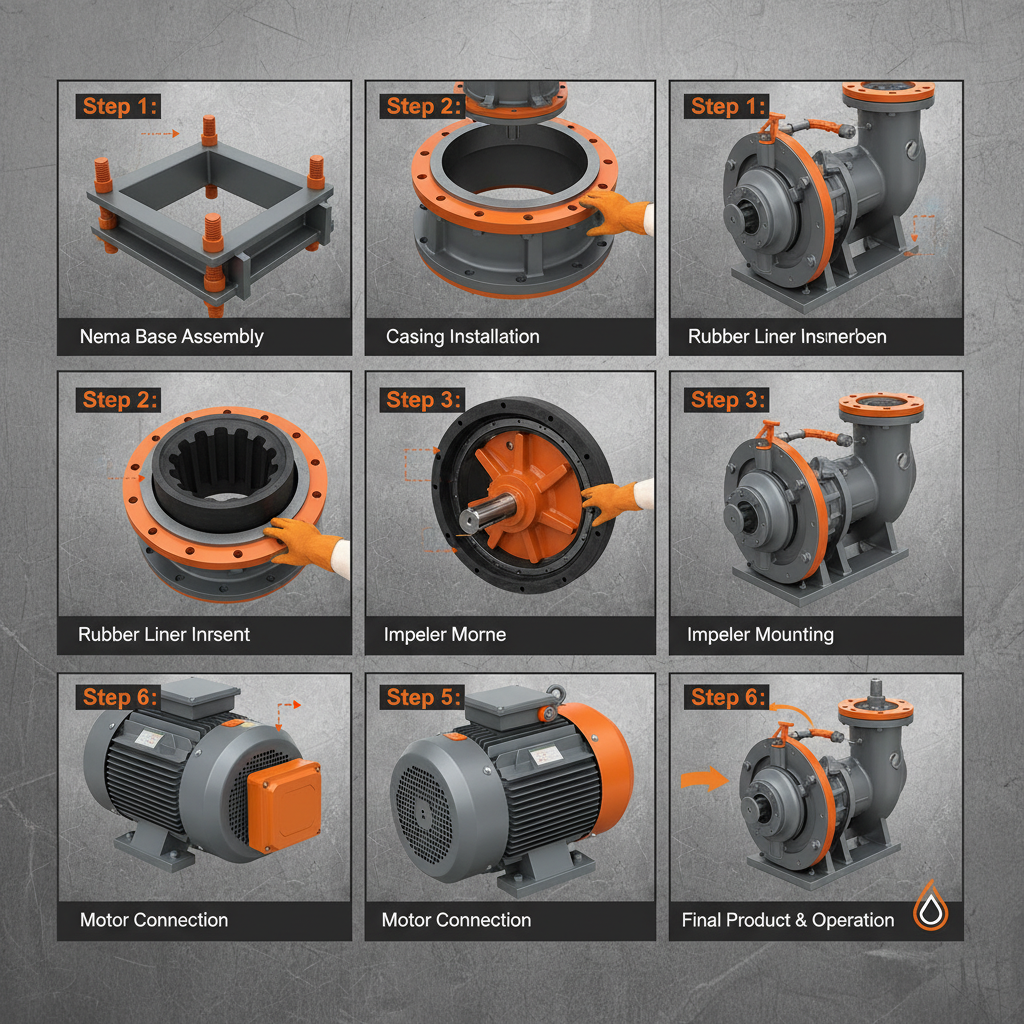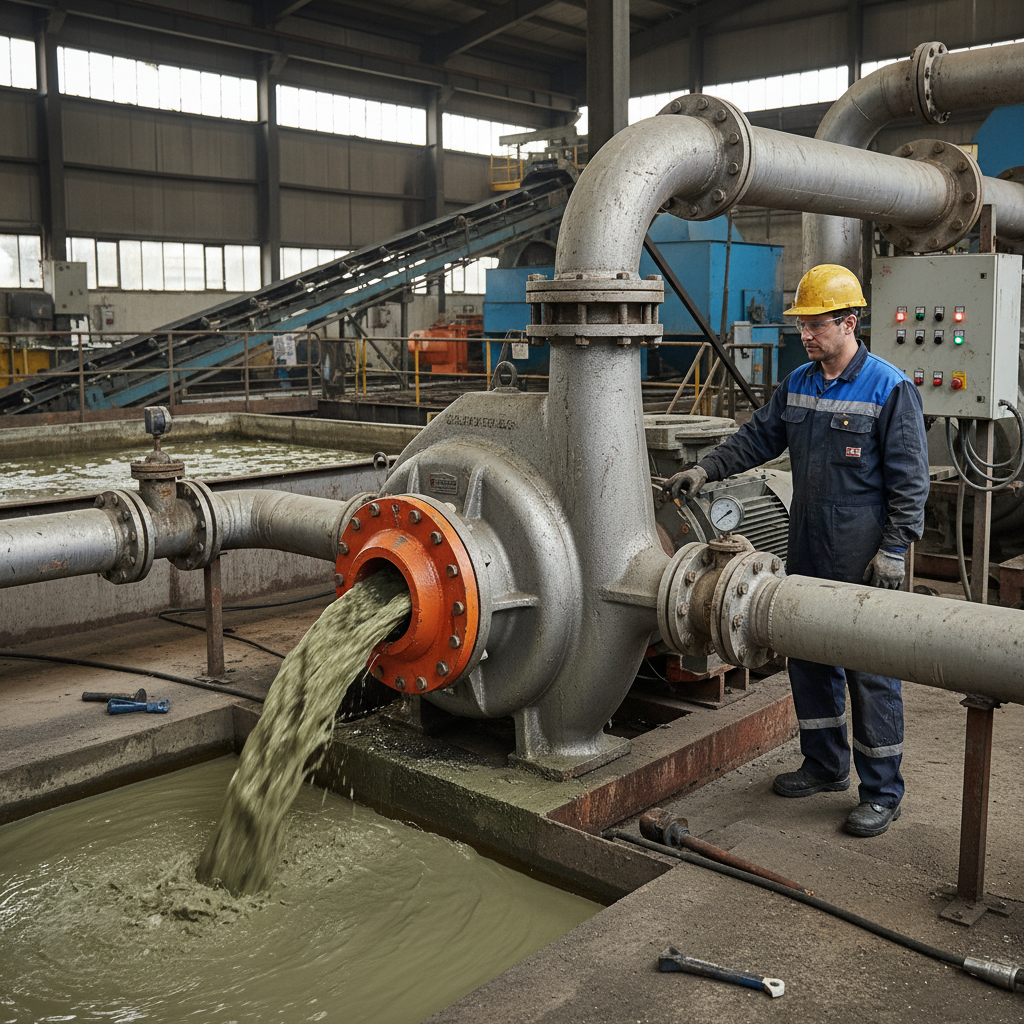
Slurry pump manufacturers play a critical role in a vast array of industries, from mining and mineral processing to wastewater treatment and chemical handling. These specialized pumps are engineered to move abrasive, corrosive, and high-solids content fluids – “slurries” – efficiently and reliably. The demand for robust and effective slurry pump solutions is consistently growing alongside industrial expansion and increasingly stringent environmental regulations. This article explores the world of slurry pump manufacturers, detailing key aspects, applications, future trends, and addressing common challenges. slurry pump manufacturer are essential for efficient operations.
Globally, the slurry pump market is experiencing significant growth, driven by the expanding mining sector in regions like Australia, South America, and Africa. The World Bank estimates substantial investments in infrastructure and resource extraction, directly influencing the demand for these pumps. Furthermore, the increasing need for efficient wastewater treatment plants in developing nations also contributes to this growth. Understanding the nuances of slurry pump technology – from materials selection to impeller design – is crucial for optimizing performance and minimizing operational costs.
Selecting the right slurry pump manufacturer is paramount to ensuring operational efficiency, minimizing downtime, and maximizing return on investment. The ability of these manufacturers to tailor solutions to specific application requirements, coupled with their commitment to innovation and after-sales support, differentiates leading players in the market. A reliable slurry pump manufacturer can significantly impact a company's bottom line.
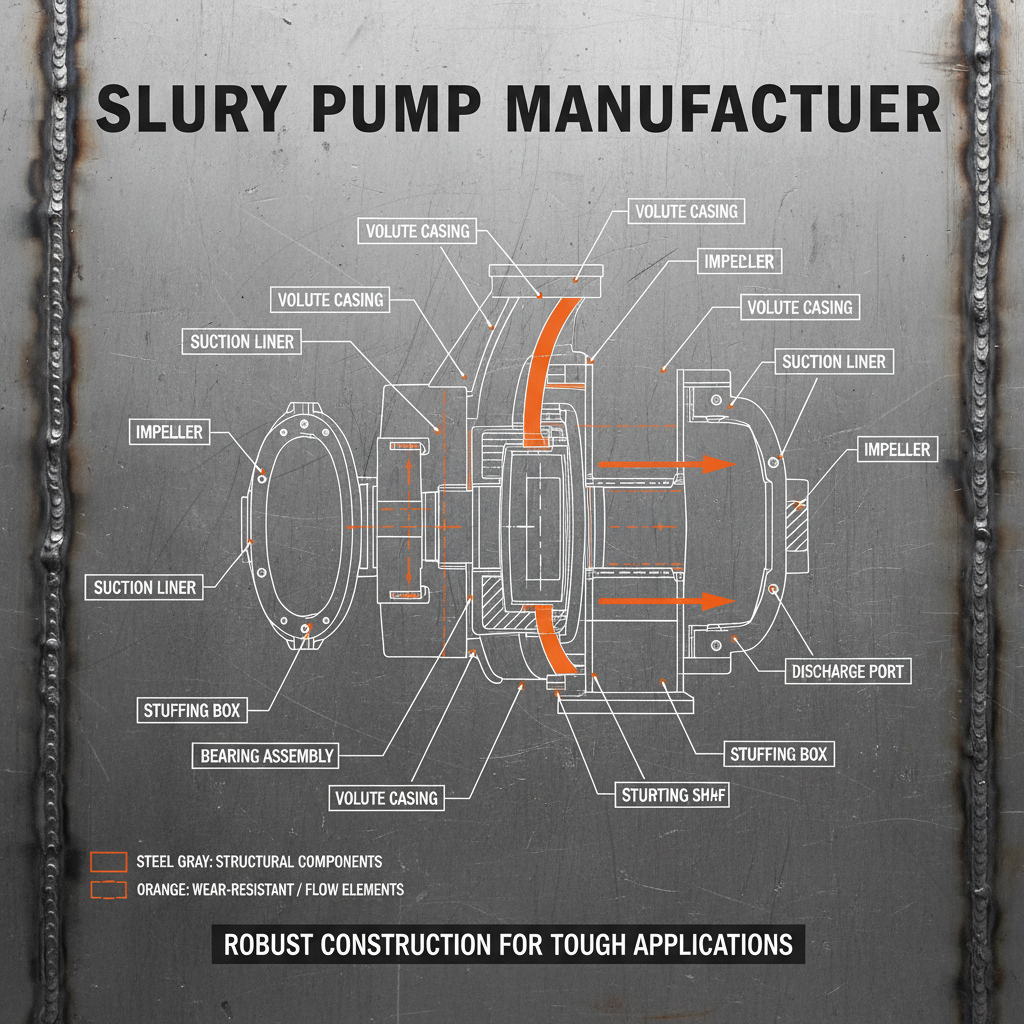

Reliable slurry pump manufacturers are vital to industries where the transport of abrasive or viscous fluids is critical. These manufacturers don’t simply build pumps; they engineer complete solutions, considering the fluid’s characteristics, the application’s demands, and the long-term operational costs. Without quality slurry pump manufacturers, industries face increased downtime, higher maintenance costs, and potentially catastrophic failures. slurry pump manufacturer plays a vital role in these industries.
A skilled slurry pump manufacturer understands the intricacies of materials science, hydraulic design, and wear resistance. They use this knowledge to develop pumps capable of handling the most demanding applications, extending pump life and reducing the total cost of ownership for their clients.
Slurry pumps are commonly constructed from high-chrome iron, due to its exceptional abrasion resistance. Stainless steel is used in corrosive applications, while rubber linings provide protection against both abrasion and corrosion. The specific material chosen depends heavily on the slurry’s composition and operating conditions. A reputable slurry pump manufacturer will advise on the optimal material selection.
Determining the correct pump size requires careful calculation of the required flow rate and head. This involves considering the slurry’s density, viscosity, and the vertical lift required. Factors like pipe friction and system pressure also need to be accounted for. Consulting with an experienced slurry pump manufacturer can ensure accurate sizing and optimal performance.
Regular maintenance for slurry pumps includes inspecting wear parts (impellers, liners, seals), lubricating bearings, and checking for leaks. Monitoring pump vibration and temperature can also help identify potential problems early on. Preventative maintenance is crucial for extending pump life and minimizing downtime.
Reducing wear and tear involves selecting the appropriate materials for the slurry’s composition, optimizing pump speed, and implementing a regular maintenance schedule. Avoiding abrasive particles in the slurry whenever possible can also significantly extend pump life. A quality slurry pump manufacturer can provide guidance on these strategies.
A VFD allows you to adjust the pump speed to match the flow rate requirements, resulting in significant energy savings. It also reduces mechanical stress on the pump, extending its lifespan. VFDs are particularly beneficial in applications with fluctuating flow demands.
Common causes of slurry pump failure include abrasive wear, corrosion, cavitation, and seal failure. Regular inspection and maintenance can help identify and address these issues before they lead to catastrophic failures. Using a reliable slurry pump manufacturer ensures the pump is designed to withstand these challenges.
Slurry pump manufacturers are integral to the functionality of numerous industries, providing the specialized equipment needed to handle challenging fluid transport applications. The selection process requires a careful consideration of slurry characteristics, performance metrics, and long-term operational costs. Investing in high-quality pumps, coupled with a proactive maintenance approach, delivers significant benefits in terms of reliability, efficiency, and sustainability. slurry pump manufacturer are key to industrial efficiency.
Looking ahead, the slurry pump industry will continue to evolve, driven by advancements in materials science, digital technologies, and a growing emphasis on sustainability. Partnering with an innovative and reliable slurry pump manufacturer is crucial for staying ahead of these trends and maximizing the value of your pumping systems. Visit our website: www.aierpumps.com.