The efficient transport of abrasive materials is a cornerstone of modern industrial processing, where the ability to move dense, particulate-laden fluids determines the overall productivity of a plant. A multistage slurry pump serves as a critical engineered solution for applications requiring higher head pressures than a single-stage pump can provide, ensuring that heavy solids reach their destination without settling or causing excessive pipe wear.
Across the globe, industries such as mining, mineral processing, and wastewater management face the constant challenge of equipment erosion and energy inefficiency. By integrating multiple impellers in series, these specialized pumping systems can elevate abrasive slurries to significant heights or over long distances, overcoming the physical limitations of standard centrifugal pumps while maintaining a manageable footprint.
Understanding the operational mechanics and material science behind the multistage slurry pump is essential for engineers looking to reduce downtime and optimize total cost of ownership. From selecting the right high-chrome alloys to optimizing flow rates, the right configuration ensures sustainable production and environmental compliance in the most demanding industrial zones.
Global Relevance of Multistage Slurry Pumping
In the current global industrial landscape, the demand for mineral extraction and waste treatment has surged, necessitating more robust fluid handling systems. The adoption of the multistage slurry pump has become vital for projects in remote regions of Australia, South America, and Africa, where deep-pit mining requires transporting tailings over extreme vertical gradients.
Failure to utilize appropriate multistage technology often leads to catastrophic pipe bursts or pump seizures, which can cost operators millions in lost production. By adhering to ISO standards for abrasive fluid transport, industries are now pivoting toward these high-head solutions to ensure a steady flow of materials while minimizing the carbon footprint associated with multiple smaller booster stations.
Defining the Multistage Slurry Pump Architecture
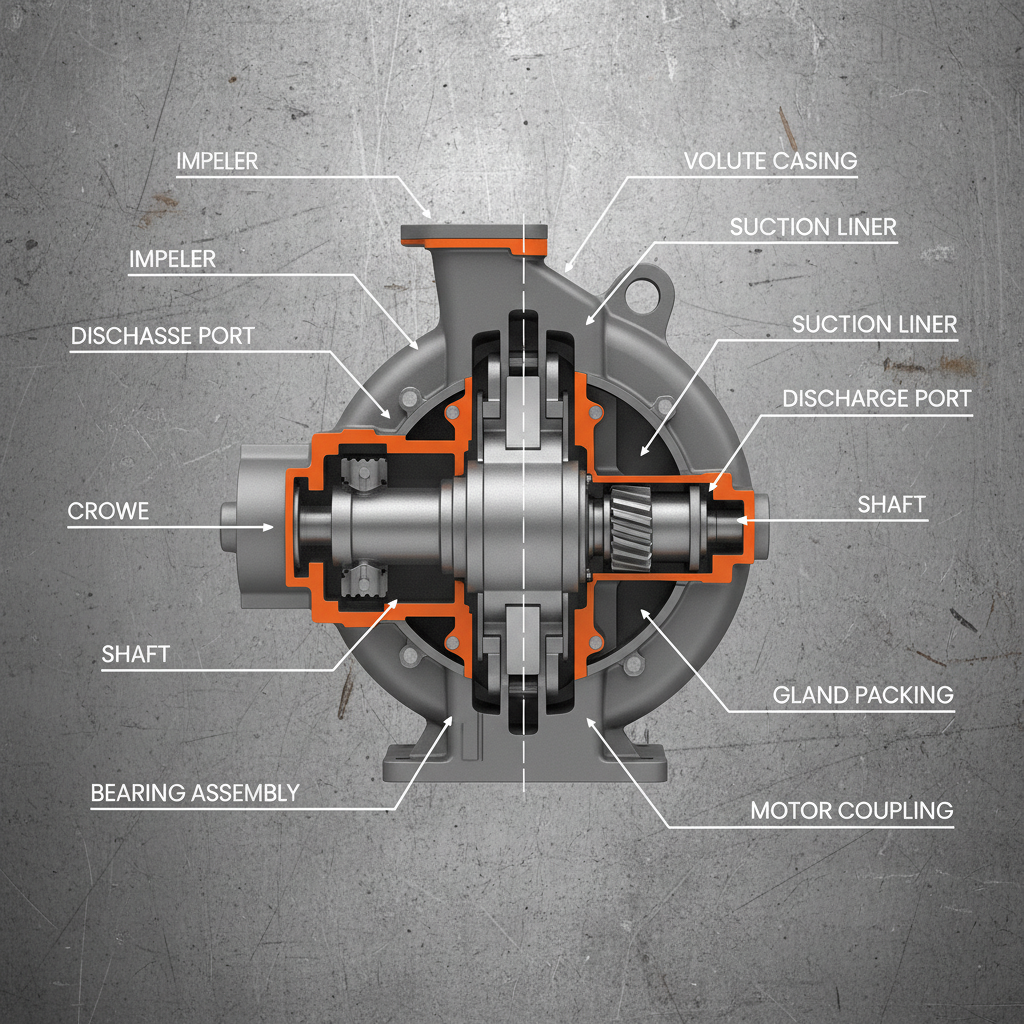
At its most basic level, a multistage slurry pump is a centrifugal pump that incorporates two or more impellers arranged in series on a single shaft. Instead of the fluid exiting the pump after one impeller, it is passed from the discharge of the first impeller into the suction of the second, effectively compounding the pressure (head) with every stage.
This architecture is specifically designed to handle "slurries"—fluids containing suspended solid particles. Unlike clean water pumps, these machines must balance the need for high pressure with the necessity of maintaining a flow velocity high enough to prevent solids from settling, which would otherwise lead to blockages and mechanical failure.
Modern industrial needs, particularly in the transition toward sustainable mining and urban sewage reclamation, require pumps that can handle varying concentrations of solids without sacrificing efficiency. This makes the multistage design indispensable for complex hydraulic circuits where a single-stage pump would simply be unable to overcome the system's total dynamic head.
Core Components for Maximum Durability
The longevity of a multistage slurry pump depends heavily on its material composition. High-chrome alloys and specialized ceramics are typically employed for the impellers and liners to combat the relentless abrasive force of particles like silica, iron ore, or gravel.
Sealing technology is another critical factor; advanced mechanical seals and gland packing are integrated into the multistage slurry pump to prevent the abrasive medium from leaking into the bearing housing, which would otherwise cause rapid mechanical degradation.
Furthermore, the shaft design must be engineered to withstand both the torsional stress of driving multiple impellers and the lateral vibrations caused by non-homogeneous slurry flows. Precision balancing of each stage ensures that the pump operates smoothly, extending the mean time between maintenance (MTBM).
Performance Metrics and Scalability
When evaluating a multistage slurry pump, the primary metrics are total dynamic head (TDH) and volumetric efficiency. The ability to scale the number of stages allows engineers to customize the pump's lift capacity to the specific topography of the site, ensuring that the fluid maintains a critical velocity to avoid sedimentation.
Scalability also refers to the ability to handle varying slurry densities. A well-designed system can maintain consistent flow rates even as the percentage of solids increases, which is vital during the peak phases of mining operations or during heavy rain events in sewage management.
Efficiency Comparison of Slurry Pumping Methods
Industrial Applications Across Global Sectors
In the mining sector, the multistage slurry pump is the workhorse for tailings management. These pumps transport waste materials from the processing plant to distant tailings dams, often across rugged terrain where multiple booster stations would be too expensive to maintain.
Beyond mining, these pumps are extensively used in the chemical processing and FGD (Flue Gas Desulfurization) industries. In power plants, they move gypsum slurries and lime mixtures, providing the high head necessary to circulate these abrasive fluids through scrubbers to remove pollutants from exhaust gases.
Long-Term Value and Sustainability
Investing in a high-quality multistage slurry pump provides significant long-term economic value by reducing the frequency of unplanned shutdowns. While the initial capital expenditure may be higher than simpler pumps, the reduction in spare parts consumption and labor costs for repairs creates a lower total cost of ownership.
From a sustainability perspective, these pumps contribute to "green mining" by enabling more efficient water recycling. By effectively moving slurries to recovery plants, mines can reclaim water and reduce their reliance on local freshwater sources, which is critical in arid regions.
Moreover, the reliability of these systems ensures a safer working environment. By automating the transport of hazardous or heavy slurries, companies reduce the need for manual handling and the risk of leaks, fostering a culture of safety and operational excellence.
Future Innovations in Slurry Transport
The next generation of the multistage slurry pump is being shaped by the digital transformation. IoT integration is allowing for real-time vibration and wear monitoring, enabling predictive maintenance schedules that replace parts just before they fail, rather than on a fixed calendar basis.
Material science is also evolving, with the introduction of nano-ceramic coatings that offer unprecedented resistance to abrasion and corrosion. These materials allow pumps to handle even more aggressive chemical slurries without the rapid degradation seen in traditional high-chrome alloys.
Finally, the move toward Variable Frequency Drives (VFDs) is optimizing energy consumption. By adjusting the pump speed to match the actual slurry density and flow requirements in real-time, operators can significantly reduce energy waste and extend the mechanical life of the pump.
Comparative Analysis of Multistage Slurry Pump Configurations
| Config Type |
Wear Resistance |
Head Capacity |
Energy Efficiency |
| Standard High-Chrome |
8/10 |
High |
7/10 |
| Ceramic Lined |
10/10 |
Medium-High |
8/10 |
| Rubber Lined (Soft) |
7/10 |
Medium |
6/10 |
| VFD Optimized |
8/10 |
Variable |
10/10 |
| Hybrid Alloy |
9/10 |
High |
8/10 |
| Custom OEM Build |
9/10 |
Very High |
9/10 |
FAQS
The primary advantage is the ability to generate significantly higher discharge pressure (head). While a single-stage pump is limited by the diameter and speed of one impeller, a multistage slurry pump uses multiple impellers in series to incrementally increase the fluid's pressure, allowing for the transport of abrasive materials over much greater distances or heights without needing multiple separate pumping stations.
Prevention is achieved by maintaining the "critical carrying velocity." Engineers calculate the minimum flow speed required to keep particles suspended based on the slurry's density and particle size. By optimizing the impeller design and pump speed in a multistage slurry pump, the system ensures that the fluid velocity never drops below this threshold, preventing sedimentation and blockages.
For extreme abrasion, high-chrome white irons (typically 27% Cr) are the industry standard due to their hardness. For corrosive slurries, duplex stainless steels or ceramic linings are preferred. Many multistage slurry pump manufacturers offer hybrid options where the most high-wear areas are reinforced with tungsten carbide or specialized ceramics to maximize service life.
Maintenance intervals vary based on the abrasive nature of the slurry. However, with modern predictive monitoring and the use of high-grade alloys, many systems operate for 6-12 months before requiring liner or impeller replacements. Regular inspections of the mechanical seals and bearings are usually conducted monthly to prevent catastrophic failure.
Yes, provided the pump is sized correctly for the maximum expected density. Using a Variable Frequency Drive (VFD) allows the operator to adjust the pump's RPM to accommodate changes in slurry concentration, ensuring that the pump remains efficient and the flow remains stable regardless of the solids-to-liquid ratio.
Air entrainment can lead to cavitation and a significant drop in efficiency. In a multistage slurry pump, air pockets can disrupt the pressure build-up between stages. This is typically managed by installing air release valves at high points in the piping and ensuring the pump is properly primed and flooded before startup.
Conclusion
The multistage slurry pump stands as a pinnacle of industrial engineering, bridging the gap between the need for high-pressure transport and the challenges of abrasive fluid dynamics. By combining advanced material science with a strategic series-impeller architecture, these pumps enable the global mining and processing industries to operate more efficiently, sustainably, and safely. From reducing operational downtime through high-chrome alloys to optimizing energy use via VFDs, the long-term value of these systems is undeniable.
As we move toward a future of smarter, more sustainable industrial operations, the integration of IoT and nano-materials will further enhance the reliability of slurry transport. For companies looking to optimize their fluid handling and reduce the total cost of ownership, investing in high-performance multistage technology is no longer optional—it is a strategic necessity. Visit our website to learn more about our solutions: www.aierpumps.com