In the demanding world of industrial mineral processing and waste management, the efficiency of fluid transport determines the viability of an entire operation. A medium head heavy duty slurry pump serves as the critical heartbeat of these systems, engineered specifically to move abrasive, high-density fluids that would destroy standard pumping equipment within hours. By balancing the pressure required to move materials over significant distances (medium head) with the ruggedness needed to withstand constant erosion (heavy duty), these machines ensure continuous production cycles in the harshest environments.
Globally, the reliance on high-performance slurry handling has intensified as mining depths increase and environmental regulations regarding tailings management become more stringent. The ability to maintain a consistent flow of ore, gravel, or chemical sludge without frequent unplanned downtime is not just a technical advantage—it is a financial imperative. Understanding the nuances of pump selection, from impeller geometry to material hardness, allows operators to optimize their Total Cost of Ownership (TCO) while maximizing throughput.
Whether it is used in a large-scale gold mine in Australia or a wastewater treatment plant in Europe, the medium head heavy duty slurry pump represents a fusion of hydraulic science and material engineering. This guide explores the technical foundations, global applications, and future innovations of these essential machines, providing a comprehensive overview for engineers and procurement specialists seeking to enhance their operational reliability.
Global Relevance and Industry Context of Slurry Pumping
The global industrial landscape is currently facing a dual challenge: the need for higher mineral yields and the pressure to adhere to strict ISO environmental standards for waste disposal. In this context, the medium head heavy duty slurry pump has become indispensable. According to industry trends, the move toward "dry stacking" of tailings—which requires pumping thicker, more abrasive slurries to higher elevations—has placed unprecedented stress on traditional pumping infrastructure, necessitating a shift toward heavy-duty designs.
Inefficiency in slurry transport often leads to pipeline blockages or catastrophic pump failure, which can cost mining operations millions of dollars per day in lost production. By implementing robust, medium-head solutions, companies can achieve a more stable flow velocity, preventing the settling of solids while minimizing the energy consumption typically associated with ultra-high-head systems. This balance is crucial for maintaining the economic viability of remote mining sites where energy costs are volatile.
Defining the Medium Head Heavy Duty Slurry Pump
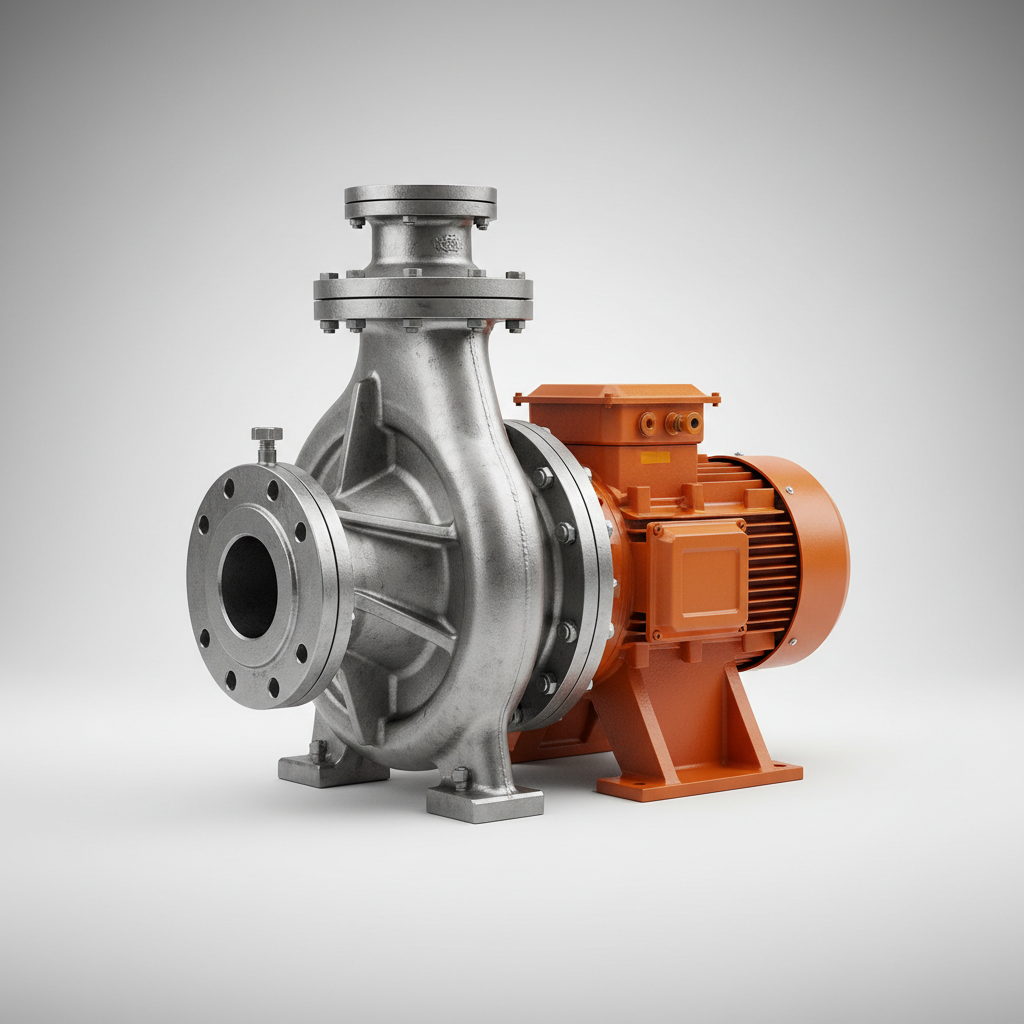
At its simplest, a medium head heavy duty slurry pump is a centrifugal machine designed to transport fluids containing high concentrations of solid particles. The "medium head" designation refers to its ability to push fluid to a moderate vertical or frictional height, typically filling the gap between low-head transfer pumps and high-pressure multistage pumps. The "heavy duty" aspect signifies the use of reinforced casings and wear-resistant liners that can withstand the constant bombardment of abrasive particles.
Unlike standard water pumps, these machines are engineered to handle "non-Newtonian" fluids—liquids whose viscosity changes under stress. This requires a specific impeller design that reduces turbulence and prevents the solids from "sandblasting" the internal components. The synergy between the motor power and the hydraulic design ensures that the pump can maintain a critical carrying velocity, keeping the solids suspended in the liquid phase throughout the transport process.
Beyond industrial utility, these pumps play a vital role in humanitarian and environmental efforts. For instance, in large-scale land reclamation or post-disaster dredging operations, the ability to move massive volumes of silt and debris efficiently is essential for restoring infrastructure. Thus, the technology transcends simple profit-making and enters the realm of critical civil engineering and environmental restoration.
Core Components and Engineering Factors
The durability of a medium head heavy duty slurry pump begins with its material selection. High-chrome alloys and natural rubber liners are the primary defenses against abrasive wear. While chrome is ideal for sharp, hard particles (like quartz), rubber is often preferred for softer, more rounded particles, as it absorbs the impact of the slurry rather than resisting it through hardness alone.
Another critical factor is the impeller geometry. A medium head heavy duty slurry pump must balance the flow rate (capacity) with the pressure (head). Open or semi-open impellers are typically utilized to prevent clogging by larger solids, while the vane angle is precision-engineered to minimize internal recirculation, which is a leading cause of localized wear and efficiency loss.
Finally, the sealing system—particularly the gland packing or mechanical seals—must be robust enough to prevent the abrasive slurry from leaking into the bearing housing. Advanced expeller seals are often integrated into these pumps to create a centrifugal barrier, throwing the slurry away from the shaft seal and significantly extending the mean time between maintenance (MTBM).
Performance Metrics and Efficiency Analysis
Evaluating a medium head heavy duty slurry pump requires looking beyond simple flow rates. The most critical metric is the "wear life" relative to the "hydraulic efficiency." A pump that is highly efficient but wears out in two weeks is less valuable than a slightly less efficient pump that lasts six months. This trade-off is the central challenge of slurry engineering.
Additionally, the Net Positive Suction Head (NPSH) is a vital consideration. Because slurry is denser than water, the risk of cavitation is higher. If the pressure at the suction side drops too low, vapor bubbles form and collapse violently, causing pitting on the impeller. A well-designed medium head pump optimizes the suction nozzle geometry to ensure a smooth transition of the heavy fluid into the pump casing.
Efficiency Comparison of Medium Head Heavy Duty Slurry Pump Configurations
Global Applications and Industrial Use Cases
The versatility of the medium head heavy duty slurry pump allows it to be deployed across diverse sectors. In the mining industry, these pumps are the workhorses of the thickener underflow, moving concentrated minerals from settling tanks to filtration plants. In the power generation sector, they are used in Flue Gas Desulfurization (FGD) systems to transport gypsum slurry, ensuring that emissions are cleaned while byproduct waste is handled efficiently.
Beyond these, the dredging industry relies on these pumps for harbor maintenance and coastal protection. For example, in Southeast Asia, where monsoon seasons lead to heavy sedimentation in shipping channels, medium head pumps are used to remove sand and silt without the need for excessive power consumption. Similarly, in the chemical processing industry, they handle aggressive waste slurries that would corrode standard stainless steel equipment, proving their value in both abrasive and corrosive environments.
Long-Term Value and Operational Advantages
Investing in a high-quality medium head heavy duty slurry pump provides tangible long-term value by reducing the "hidden costs" of operation. While a cheaper pump may have a lower initial purchase price, the cost of frequent impeller replacements, labor for downtime, and lost production often far exceeds the initial investment in a premium, heavy-duty model.
From a sustainability perspective, these pumps contribute to a lower carbon footprint by optimizing energy usage. Modern hydraulic designs reduce the "internal slip" of the fluid, meaning more of the electricity used by the motor is converted into actual fluid movement. This energy efficiency, combined with longer component lifespans, reduces the amount of scrap metal and industrial waste generated by the facility.
Furthermore, the reliability of these systems enhances workplace safety. Pump failures in slurry lines often lead to leaks or pipe bursts, which can be hazardous to personnel and the surrounding environment. By ensuring a stable, leak-free operation, companies can foster a safer working environment and maintain a stronger reputation for corporate responsibility and operational excellence.
Future Trends in Slurry Handling Technology
The future of the medium head heavy duty slurry pump is being shaped by the digital transformation of the mining and manufacturing sectors. The integration of IoT sensors—measuring vibration, temperature, and flow rate in real-time—is enabling "predictive maintenance." Instead of replacing parts on a fixed schedule, operators can now replace a liner exactly when it reaches its wear limit, eliminating unnecessary downtime.
Material science is also evolving. We are seeing the emergence of nanostructured ceramics and hybrid composite liners that combine the hardness of chrome with the elasticity of rubber. These materials promise to further extend the life of pump internals, potentially doubling the interval between overhauls and reducing the overall cost per ton of material moved.
Finally, there is a growing shift toward variable speed drives (VSDs). By allowing the medium head heavy duty slurry pump to adjust its speed based on the slurry density, operators can maintain the critical carrying velocity while slashing energy costs during periods of lower throughput. This move toward automation and intelligence marks the next chapter in industrial fluid handling.
Comparative Analysis of Slurry Pump Technical Specifications
| Pump Series |
Max Head (m) |
Wear Life (Hours) |
Efficiency Rating |
| Standard Heavy Duty |
45 |
4,000 |
7.2 |
| High-Chrome Series |
50 |
8,500 |
7.8 |
| Rubber Lined Series |
40 |
6,000 |
7.5 |
| Ceramic Composite |
55 |
12,000 |
8.1 |
| Variable Speed Opti |
48 |
7,000 |
9.2 |
| OEM Custom Build |
60 |
10,000 |
8.5 |
FAQS
The primary difference lies in the pressure capabilities and the impeller design. A medium head pump is designed for moderate lift and distance, typically offering a better balance between flow volume and pressure. High head pumps are designed for extreme vertical lifts and use higher rotational speeds or multiple stages, which often increases wear and energy consumption. For most industrial mineral processing tasks, a medium head heavy duty slurry pump provides the most cost-effective efficiency.
The choice depends on the nature of the solids in your slurry. High-chrome alloys are superior for "hard" abrasion, where the slurry contains sharp, jagged particles (like silica or ore) that would slice through rubber. Natural rubber liners are ideal for "fine" abrasion or softer materials, as they absorb the impact of the particles, leading to a longer lifespan in applications like sand pumping or tailings management.
Yes, provided the materials of construction are compatible with the chemicals involved. While standard heavy-duty pumps focus on abrasion, specialized versions use corrosion-resistant alloys or specialized polymers to handle acidic or alkaline slurries. It is critical to specify the pH level and chemical composition of your fluid to ensure the pump casing and seals are correctly specified for the environment.
The most common causes are operating the pump too far from its Best Efficiency Point (BEP) and allowing the flow velocity to drop below the "critical carrying velocity." When the velocity is too low, solids settle and create "sand-blasting" zones. To prevent this, use variable speed drives to maintain optimal flow and ensure the pump is correctly sized for the slurry density and viscosity of your specific application.
Inspection intervals vary by application, but for heavy-duty operations, a monthly check of the pump's performance (flow vs. pressure) is recommended. A drop in head usually indicates significant wear in the impeller or casing. Many modern facilities now use ultrasonic thickness gauges to measure liner wear without dismantling the pump, allowing for planned maintenance rather than reactive repairs.
Absolutely. Modern medium head heavy duty slurry pumps utilize Computational Fluid Dynamics (CFD) to optimize the internal flow paths, significantly reducing turbulence and energy loss. When paired with a Variable Frequency Drive (VFD), these pumps can reduce energy consumption by 20-40% compared to older, single-speed pumps by adjusting output to match the real-time demand of the process.
Conclusion
The medium head heavy duty slurry pump is more than just a piece of industrial hardware; it is a critical engineering solution that enables the global extraction and processing of vital minerals. By balancing hydraulic power with extreme wear resistance, these pumps allow industries to operate in the most challenging environments while maintaining economic viability and operational safety. From the selection of high-chrome alloys to the integration of IoT-driven predictive maintenance, the evolution of this technology continues to drive efficiency across the mining, dredging, and chemical sectors.
As we look toward a future of sustainable mining and smarter industrialization, the role of high-efficiency slurry handling will only grow. For companies seeking to optimize their production lines, the focus should remain on the Total Cost of Ownership—prioritizing durability, energy efficiency, and professional engineering over initial cost. By investing in robust pumping solutions today, operators can ensure long-term reliability and a competitive edge in an increasingly demanding global market. For more professional guidance and high-performance equipment, visit our website: www.aierpumps.com.